Resin traceability at Hubbell
Situation: Resin traceability in a critical process
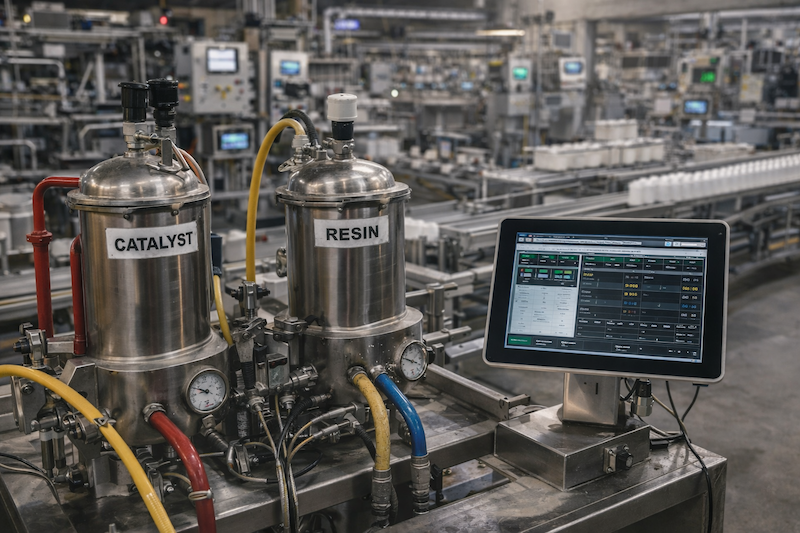
At Hubbell's plant in Ciudad Juárez, controlling consumption and dosage was key to protecting quality and costs. The challenge was to transform the process into a measurable system with reliable data by SKU, station, mixer, and shift. This case study demonstrates how resin traceability went from being a blind spot to a source of operational and financial decisions, with real-time monitoring and audit-ready reports.
Hubbell operates in an environment where resin and catalyst directly impact product conformity and cost per piece. However, the available information did not provide sufficient visibility to know what was actually being consumed at each station, nor to compare actual consumption against the recipe/BOM. The goal was to implement complete resin traceability, with consistent data for production, quality, and inventory.
Problems and needs: When resin traceability is unreliable
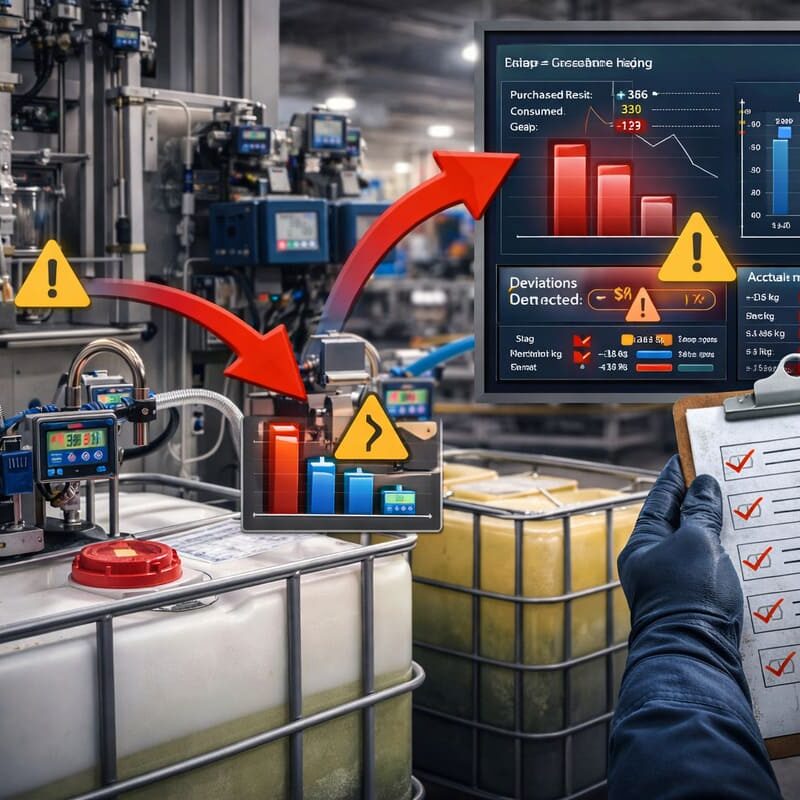
The first symptom was a discrepancy: differences between resin purchased and resin recorded as used, without a clear cause. Furthermore, dosage deviations from the recipe/BOM were detected by SKU, impacting quality and resulting in waste. Finally, there was no detailed traceability by mixer, operator, and shift. The need was clear: real-time resin traceability, with control by SKU and automated reports.
Key needs
Reasons: Why opt for real-time resin traceability
The priority was to eliminate decisions based on estimates and replace them with verifiable data. With resin traceability, Hubbell aimed to reduce unidentified losses, ensure correct dosing per SKU, and improve cost control per product. It was also necessary to connect operations with management so that inventory and production spoke the same language. In short: less uncertainty and a greater ability to act quickly in response to deviations.
Capabilities: What was implemented to ensure resin traceability
The solution was designed to consolidate resin traceability and operational control into a single workflow, integrating the dispensing environment (SCADA) with the management layer (ERP/SAP). Real-time monitoring was enabled with indicators per mixer and metrics comparable to the Bill of Materials (BOM). In addition, administrative and scrap capture functions were incorporated, along with a robust reporting layer for traceability, defects, and OEE.
Featured Capabilities
Main screen with real-time monitoring: mixer status, production and OEE.
Operational record: goals per shift and scrap capture with calculation according to recipe.
Catalogs and administration: families, groups, mixers, shifts, molds and defects.
Reports: traceability, defects and OEE with filters by shift.
Results: Direct impact of resin traceability on control and costs
With the implementation, resin traceability allowed for monitoring consumption from day one and detecting deviations before they resulted in losses. Teams gained visibility by station and by shift, which accelerated decision-making and reduced reliance on manual records. At the management level, the reports facilitated auditing and analysis, improving planning and financial control of consumption by SKU.
Key results
Elimination of 100% of physical logs and manual tours.
Asset protection and operation within recommended curves.
Reduction of human errors through automated tracking.
Improved operational and financial analysis with automated reports.
Early detection of anomalies and a basis for continuous improvement.
Originally published on March 17, 2026, updated on June 1, 2026